Looking for a reliable Neutral Spirits supplier?
Contact our team to discuss your specifications and volume requirements.
Our Neutral Spirits / Extra Neutral Alcohol (ENA) are high-purity ethanol products designed for applications where a clean, neutral odor profile and consistent quality are essential. With purity levels of up to 99.87% v/v, ENA provides dependable performance across a wide range of formulations and manufacturing processes.
Neutral Spirits are refined ethanol products with a highly neutral character. Their low-congener profile makes them particularly suitable for applications where the presence of odor or impurities could affect the final product. Our ENA can be supplied according to customer requirements, making it suitable for both standard and specialized industrial applications.
Used as a carrier and solvent in fragrance and perfume formulations.
Suitable for selected cosmetic, skincare, and personal-care formulations where high-purity ethanol is required.
Can be used as a solvent or carrier for selected aroma and flavor formulations, subject to applicable requirements.
Used in various solvent, blending, and manufacturing processes.
Contact our team to discuss your specifications and volume requirements.
Our Absolute Alcohol / Anhydrous Alcohol (AAE) is high-purity ethanol designed for applications where moisture content needs to be tightly controlled. With less than 0.5% water, Absolute Alcohol is suitable for specialized chemical processes, laboratory applications, pharmaceutical processes, and other applications where excess moisture can influence reactions, formulations, or product performance.
Unlike standard ethanol grades, Absolute Alcohol is processed to achieve a significantly lower water content. This makes it particularly useful in moisture-sensitive applications where water can interfere with chemical reactions or affect the stability and performance of a formulation.
Used as a solvent and processing material in laboratory and research environments.
Suitable for chemical processes where controlled moisture levels are important.
Can be used in selected pharmaceutical manufacturing and formulation processes according to applicable specifications.
Suitable for specialized manufacturing processes requiring low-water ethanol.
Speak with our technical team about the required specification.
Our Denatured Ethanol (DEN) is formulated for industrial and technical applications using selected denaturants appropriate to the intended use and applicable regulatory requirements. We understand that different industries require different specifications. Therefore, our denatured ethanol solutions can be developed around your application, process requirements, handling conditions, and regulatory framework.
Denatured ethanol is ethanol containing approved denaturing substances that make it unsuitable for beverage consumption while retaining its usefulness for industrial and technical purposes. The choice of denaturant can vary depending on the application and local regulatory requirements.
Used in selected cleaning and surface-treatment applications.
Suitable for processes requiring ethanol-based solvent properties.
Can be incorporated into various industrial manufacturing processes.
Suitable for specific technical and chemical applications.
We can help determine the appropriate Denatured Ethanol specification.
Our Rectified Spirit (RS) is a refined ethanol product designed for general-purpose industrial applications. It offers consistent quality and dependable performance across blending, cleaning, solvent, extraction, and other technical processes. With flexible supply options and application-focused specifications, our Rectified Spirit can support both routine and specialized industrial requirements.
Rectified Spirit is produced through controlled purification processes to achieve a refined alcohol suitable for a wide range of industrial uses. Its versatility makes it a practical choice for manufacturers and processors looking for a dependable ethanol-based material.
Used as an alcohol component in selected industrial formulations and blending processes.
Suitable for applications requiring ethanol-based cleaning properties.
Can be used as a solvent in suitable industrial processes.
Used in selected extraction and processing applications.
Contact us with your required grade and volume.
Our Pharma & Lab Grade (PHM) ethanol is designed for applications where tighter quality control and consistent product characteristics are important. These products are evaluated against key parameters such as odor, colour, specific gravity, and impurity profile, helping customers select an ethanol grade appropriate for their specific pharmaceutical, laboratory, research, or technical application.
Pharmaceutical and laboratory applications often require greater control over raw-material quality and consistency. Our PHM grade is supplied with a focus on controlled specifications and quality assurance. The exact specification can be established according to the intended application and applicable standards.
Suitable for selected pharmaceutical manufacturing and formulation processes.
Used in laboratory preparation, processing, and analytical applications.
Suitable for controlled laboratory and R&D environments.
Can be used where consistent ethanol quality is required.
Discuss your pharmaceutical or laboratory requirements with our team to identify the appropriate ethanol specification.
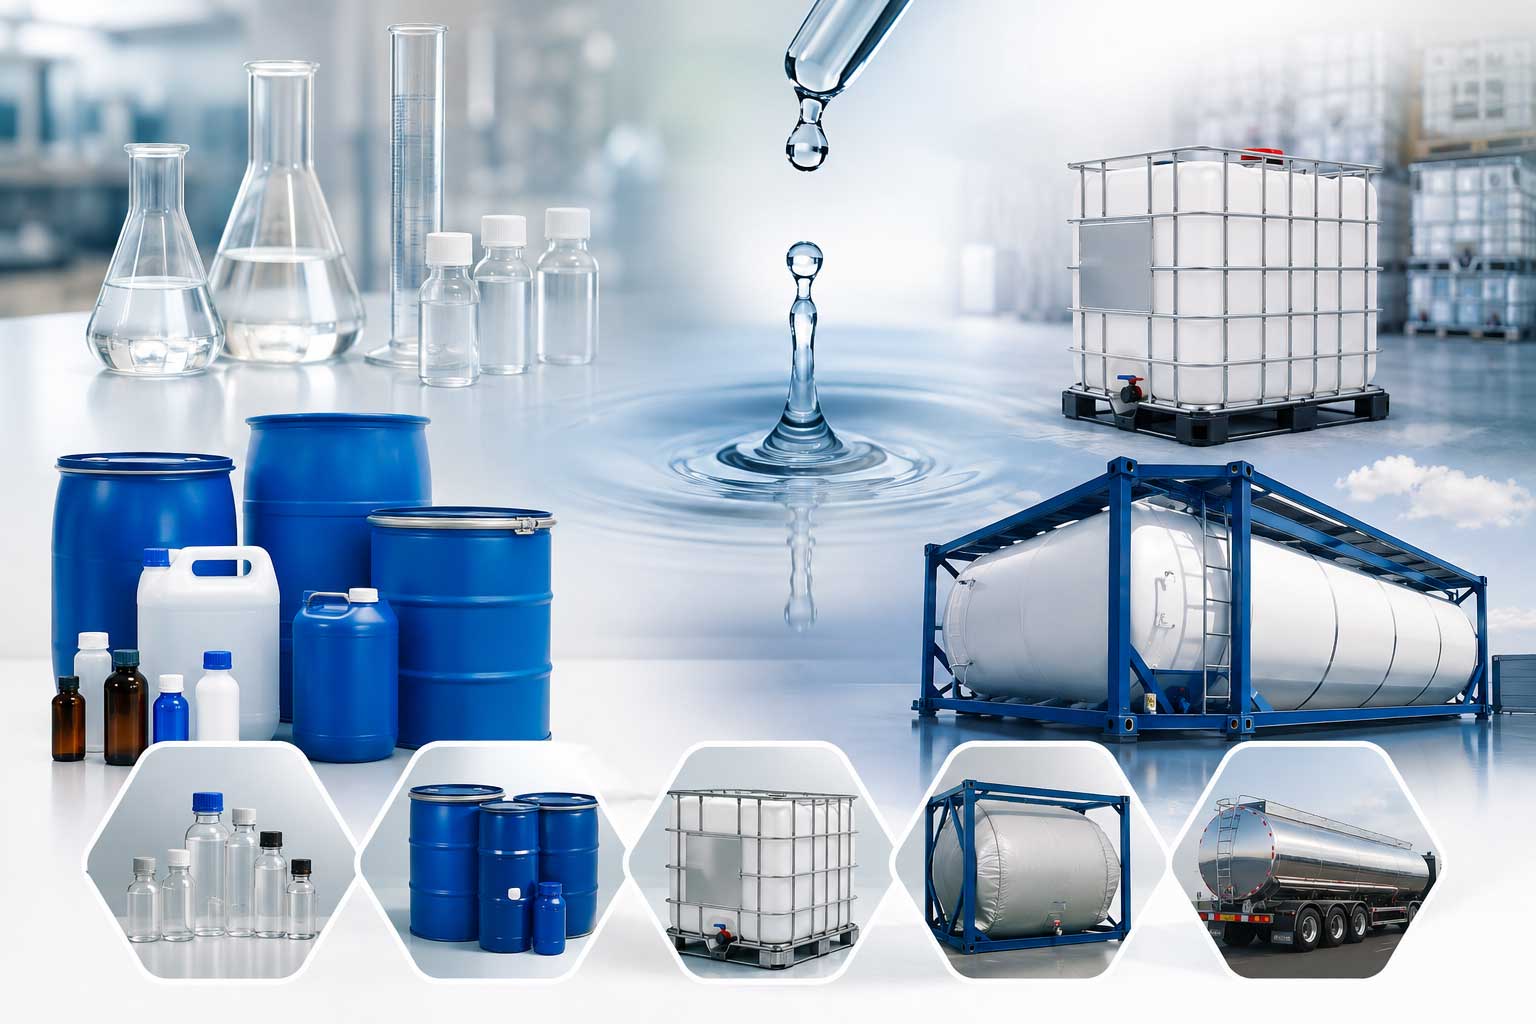
Every customer has different product specifications, quantities, handling requirements, and logistics needs. Our Custom Blends & Packaging service provides flexible solutions designed around your individual requirements. From customized ethanol blends to specialized packaging formats, we can support customers with solutions tailored to their application and supply-chain needs.
Our blending solutions can be developed around requirements such as ethanol concentration, water content, denaturant requirements, application-specific specifications, packaging volume, and transportation requirements.
Suitable for customers requiring manageable quantities for specialized applications.
Efficient for medium-volume industrial requirements.
Suitable for larger-volume liquid transportation.
Designed for efficient bulk transportation and high-volume industrial supply with capacities from 250 ML up to 40,000 L.
Share your specifications with us and let us develop a solution tailored to your application and supply-chain requirements.
Powering industries with premium ethanol and dependable supply solutions.
© All Rights Reserved by Rudra Industries.
Website Designed by Mirackle Solutions